Online Orders Only SALE! 10% off all Freud & Diablo Products! 20% off all Techniks CNC Accessories! 10% off Sale on all Southeast Tool! We Offer Quantity Discounts with Whiteside & Viking! New Lower Prices on entire stock of Vega Tools!
Posted by Kathryn Magendie on | Comments Off on Spoil Boards, Hold-downs, and Dust Collection
Holding the part to be cut firmly and without movement or vibration is often the biggest challenge faced when cutting on a CNC. Chatter, movement, premature tool wear, tool breakage, poor edge finish, and chipping are the result of inadequate hold-down. How well you can hold the part is perhaps the biggest factor in how fast you can cut.
There is a lot of information on building dedicated spoil boards and jigs so we cover the basics in our free downloadable CNC Manual, and will provide an excerpt here. For the rest of the article, refer to the CNC Manual pages 13, 14, 15.
Some factors to consider include:
• Some CNC operations are best suited to using flow through or suck through vacuum systems. Particularly well-suited for cutting large parts and sheets of material, these types of routers utilize replaceable spoil boards—so called because they are underneath the material to be cut and are cut and “spoiled” during machining. The spoil board can then be resurfaced and used again, sparing the router table underneath from damage. These types of systems are easy to use and require minimal maintenance. Using low (LDF) or medium density fiberboard (MDF), both sides are machined level using a large “fly” cutter to remove any imperfections or coatings. Vacuum is evenly distributed to the entire surface of the table. Air loss from the sides can be minimized by using rubberized or latex paint. Areas not to be used should be sealed with sheets of laminate, plastic, or other non-porous materials. Grooves resulting from the cutting process can cause vacuum leakage when cutting a variety of patterns. Resurfacing the spoil board should be done regularly.
• Smaller or more intricate parts are better suited to dedicated spoil boards due to vibrations and part movements. Cutting small parts can be challenging since a larger volume of air is lost due to the number of channels cut between parts. As more parts are cut, more air pressure is lost, resulting in vibration and part movement.
• Leaving a thin skin (onion skin) or programming tabs at certain points can help to hold small parts together but require a secondary routing or sanding operation.
• Use dedicated spoil boards for recurring part runs. Taking the time to make a proper spoil board will pay for itself by allowing faster feed rates, giving you a better finish, and prolonging tool life.
To continue, refer to the CNC Manual pages 13, 14, 15.
Posted by Kathryn Magendie on | Comments Off on Let EOASAW Make You Custom Inserts
With insert tooling, the carbide is affixed to the tool body by the use of gibs and screws instead of being brazed / welded on. There are two basic types: dedicated insert heads and universal insert heads. With dedicated heads the body is machined to match the profile of the insert to provide support. With universal insert heads the body is open and does not provide support; instead, there is a “backing plate” that is profiled the same as the insert to provide support. With the Universal design you are able to use the same head with multiple profiles by changing the backing plate and inserts. The Universal design is generally more expensive since it consists of an additional backing plate and the inserts are in general larger to accommodate a variety of profiles. We would be happy to help you select the style that will work best for you.
Where can insert tooling best be utilized?
Insert tooling is appropriate in a wide variety of applications – just about any application where you currently use a carbide-tipped tool. There are some common profiles available that utilize standard inserts, making them very affordable. Standard Insert heads are very common on edgebanders, standard shaper cutter profiles, planer heads, and router bits. Edge of Arlington can make you custom inserts to match your unique profiles. We will assign them their own unique part number and they will be the same today, tomorrow, or years from now.
Benefits of Insert Tooling
Inserts can provide consistency in production, allowing you to maintain tight tolerances in critical operations such as cope & stick applications. Using replaceable inserts instead of brazed-on carbide allows you to maintain a constant diameter, which simplifies set-up. Insert tooling is also able to utilize harder, more wear resistant carbide than traditional CT tooling. These micro-grain carbides, while more wear resistant, tend to crack when brazed on. While the initial set cost may be more, inserts are more economical over the long run due to the carbide lasting longer. When purchasing a new profile, it is customary to have to order 9 to 12 inserts to cover production set-up costs. However, if you have a brazed cutter, you generally have to buy multiple heads in order to have a back-up for when the tool is serviced. With insert tooling, one 3-wing body and 12 inserts is equivalent to 4 brazed heads – except they should last several times longer due to the superiority of the carbide.
Limitations / Drawbacks of Insert Tooling
While very versatile in nature, the design does not lend itself well to small diameters due to the need to affix the insert with gibbs and/or screws. This is especially an issue when it comes to router bits. Furthermore, there is more user maintenance involved with insert tooling. When the inserts are changed, everything needs to be cleaned and inspected for any damage. Inserts must be properly aligned when replaced in order to maintain the profile. If the inserts are not aligned properly, one wing is going to do most of the work, resulting in distorted profiles, poor finish, loose fits for cope & sticks, or insert failure. Machinery must be well maintained in order to assure tight tolerances. If there is run-out in a cope & stick set for example, the fit is going to be loose. There is no way to adjust the fit with shims as there would be in traditional carbide-tipped stackable sets.
Posted by Kathryn Magendie on | Comments Off on Climb Cut vs. Conventional Cut
Climb and conventional cutting refer to the direction of travel in relation to spindle rotation. In the case of a right-hand rotation spindle, climb cutting (clockwise direction) can produce a different result than conventional cutting (counterclockwise direction).
• In many circumstances conventional (CCW) cutting will provide the best finish, especially in plastics and with larger diameter tools. If the scrap piece has a better finish than the finished part, a change in cutting direction will provide you with the opposite results. Don’t be afraid to experiment with cutting directions or have different cutting directions on the same workpiece.
• There are also left-handed tools and holders available for left-hand rotation—climb cutting would then become counterclockwise and conventional cutting would become clockwise.
• When cutting the interior of a part as opposed to the outside perimeter, conventional cut becomes climb cut and vice versa.
• When cutting two parts with one pass such as when cutting parts that are nested or mirrored, keep in mind that one side of the cut will be conventional cut and the other will be climb cut.
• Climb cutting is more aggressive and can move small parts.
• When cutting hard materials and metals such as aluminum, climb cutting is preferred.
Posted by Kathryn Magendie on | Comments Off on Edge of Arlington Featured on Inside The Blueprint Local Edition
Edge of Arlington Saw & Tool is featured on Inside The Blueprint.
Join us as they go behind the scenes for innovations in healthcare, design-build manufacturing, and, of course, Edge of Arlington’s segment on tooling and machinery.
Posted by Kathryn Magendie on | Comments Off on Tips to Safely & Efficiently Prolong the Life of CNC Tooling
• Dead stops, also known as “dwelling in the cut,” can lead to premature tool wear and failure. When changing directions of travel or when cutting small pieces, a one second stop at 18,000 RPM generates enormous heat and no means of extraction. Imagine rubbing your hands together 300 times per second – a sure way to a blister. This is more of a machinery and software issue. Certain programming techniques can help to compensate, such as ramping, use of loops at sharp outside corners, and the use of exit ramps.
• Plunge cutting, while this is the oldest and most widely used method of entering the material, it is not always the most efficient. Plunge cutting can lead to chips wrapping around the router bit after repeated plunges. Whenever possible you should Ramp into the cut. This eliminates the heat generated during the plunging process and can eliminate burn marks at the plunge point. Plunging can also cause the bit to “walk” because there is no centering point; this will be evident as oval holes and entry points larger than the diameter of the tool. If you cannot ramp in, a good alternative is to plunge down outside of the workpiece and enter from the side. Spiraling in can also help; whatever it takes to keep the router bit moving.
• Routing holes is never the optimum choice. Use drills for drilling, routers for routing. Drills turn at much lower RPM than routers do; router bits generate too much heat when drilling. Drilling just a couple of holes per sheet will significantly reduce the life of your tooling; in fact, you will probably dull more drilling the 2 holes than cutting the entire piece. If you do not have drill heads to take advantage of European type boring bits, turn the RPM down as low as possible, 4-5000 RPM at most, and plunge as fast as possible, an upshear will help to remove the chips if hold down is not a problem. On deep holes “pecking” can sometimes help.
• Small parts and scrap pieces can become projectiles if left after the cutting process without sufficient hold down. They can also be sucked into the dust collector and cause a blockage. Skin cutting and the use of tabs can help to hold small parts. • Over-tightening of the collet and collet nut is a common mistake. Most operators assume that the tighter the better – this is not true and can lead to premature tool and collet wear and tool breakage. Collets are the most misunderstood and overlooked part of the CNC, often the cause of poor finish, short tool life, and unnecessary machine wear. Collets are made of spring steel and are subject to distortion when put under undue pressure. It is highly recommended that collets be tightened to manufacturers’ specifications with the use of a torque wrench
• Fires, yes it happens. A tool left in the same place for a sufficient amount of time can and will start a fire. It is important never to leave a CNC running without an operator; you wouldn’t believe how fast things can go wrong. The dust collection system and the vacuum system will aid in the fires speedy travel. If this ever happens to you, beware of flash-back when the vacuum is turned off. When it is safe to do so, it is important to remove and examine the bleeder board and table underneath, embers can remain and once again flair up.
Check out our free CNC Manual available at EOASAW.com!
Our free CNC Manual will guide you through selecting the right tool, maximizing machine time, finish, tool life & profits. Here we talk about tool materials and their uses.
High speed steel (HSS). Used primarily on soft woods such as pine, aluminum, and soft plastics. HSS can be sharpened to a very sharp edge and at the appropriate hook and clearance angles “slices” through soft material, reducing pre-splitting. HSS is more impact resistant than carbide but is not wear resistant enough to hold up to many of today’s man-made materials.
Tangtung (TG) A cast alloy material with a high tungsten content. Tangtung retains its hardness at very high temperatures, is more shock resistant than carbide, and resists corrosion from wood acids. Tangtung, like HSS, can be sharpened to a fine edge and is primarily used in hardwoods for a superior cross-grain cut. TG can and has been used in insert tooling for CNC applications. Freeborn Tool has a line of insert shaper cutters available in Tangtung. Tangtung is never recommended for manmade fiber boards or plywood.
Carbide-tipped (CT). Used primarily on hard woods, laminates, composite materials, and for abrasive or resin-based products. Carbide is welded or brazed onto a steel body and profiled to the desired pattern; therefore it is the most common type of material used for profile and custom tooling. There are many different grades of carbide. The harder the grade of carbide, the more likely it is to break during the heating and cooling process in manufacturing—problems overcome with insert tooling.
Solid carbide (SC). Used primarily on hard woods, wood composites, laminates, plastics, aluminum, and other composite materials for longer life and faster feed rates. Solid carbide can be cast into just about any shape. Solid Carbide rods are well-suited for making router bits with spiral geometries and small form or profile tools. Solid carbide blanks are also well-suited for insert tooling and are available in many standard sizes and configurations. Solid carbide is very wear resistant but not impact resistant—strain and deflection often lead to tool breakage.
Diamond (PCD). Polycrystalline diamond is primarily used on composite materials such as melamine. PCD diamond is extremely heat and wear resistant (100+ times carbide) but is not impact resistant, and in fact, it chips fairly easily. Materials must be free of all foreign matter and be homogenous in nature or tool damage may result. Machine condition and maintenance are vital to cost effectiveness. High initial cost but very low operating cost can make diamond tooling a very economical alternative. Diamond wafers are brazed on to a steel body and are not suited to small sizes.
Insert tooling. Insert tooling can provide consistency in production. Using replaceable inserts instead of brazed-on-carbide allows you to maintain a constant diameter. Insert tooling is also able to utilize harder, more wear resistant carbide than traditional CT tooling. While very versatile in nature, the design does not lend itself well to small diameters due to the need to affix the insert with Gibbs and/or screws.
Posted by Kathryn Magendie on | Comments Off on Factors To Be Considered Before Selecting Your Tool
CNC Router Accessories
Many factors need to be considered when evaluating any cutting situation, before selecting a tool. You can find more useful information in our FREE CNC Manual available for download on our site!
What is the desired finish? Chip-free, hidden part, some minor chips ok, etc. Are both sides (top, bottom) of material of equal importance? The desired finish will often dictate not only what type of tool we can use but also how fast we can cut and whether we must make multiple passes.
Which is more important, speed or finish? While striving for both, sometimes we must assign priorities or make compromises. Higher quality finish can mean higher machining costs (multiple passes, use of more expensive tooling, slower feed rates, etc.). However, ironically, most people run their tools at too slow a feed rate at too high of a RPM, resulting in heat buildup and premature tool wear.
What are the machines capabilities and limitations? It is important to know your CNC’s capabilities and limitations. If your machine’s top feed speed is 600 IPM as opposed to a machine capable of feed speeds of 1200 IPM, your tool selection and setup will be quite different. It is important to note here that just because your machine is capable of running at 3400 IPM does not mean you can cut at that rate. When programming any cut for the first time, it is important to ascertain at what feed that part is to be cut. Part size or geometry alone may preclude you from running more than a few hundred IPM.
Do you have sufficient ability to hold the material you are cutting? If you can’t hold it, you can’t cut it. This is one of the most common problems that I encounter. I am continually amazed how many people will accept minimal feed rates and quality because of chatter and movement. Your ability to make a clean fast cut is related to your ability to hold the material firmly without vibration. Insufficient hold-down can be responsible for everything from premature tool wear and breakage to sub-standard parts, chatter marks, chipping, and material movement. A little planning and effort will give you huge payoffs in productivity and cost savings. When purchasing a CNC router, don’t skimp on the vacuum system. I have never met anyone who said they had too much.
What is the material you are cutting? Raw particle board, plywood, MDF, single-sided laminate, double-sided laminate, etc. Different materials have different cutting properties and may restrict your tool selection and will often dictate geometries, feed, speed, etc.
Are there any operations after this one that will cover, conceal, or change the shape of the part being cut? For example, the top edge will be rounded over or the edge will be covered in such a manner so that a small chip would be of no importance.
Is exact size important? Does another part rely on the accuracy of this part? Maintaining exacting measurements may require multiple passes after a tool is serviced or if the size is non-standard. Edge of Arlington offers insert and diamond tooling designed to solve these types of problems.
Free! CNC Manual
Part configuration and size are important considerations. Small parts can be hard to hold. Intricate parts, parts with holes, curves, and short cuts can be challenging due to heat generated because of a machinery’s inability to make instantaneous speed and directional changes. Advances in machine capabilities have greatly improved the speeds associated with travel time and the ability to change direction. However, a bit turning at 18,000 RPM still turns at 300 inches per second and a good Boy Scout can start a campfire with a stick at a much lower RPM.

 Holding the part to be cut firmly and without movement or vibration is often the biggest challenge faced when cutting on a CNC. Chatter, movement, premature tool wear, tool breakage, poor edge finish, and chipping are the result of inadequate hold-down. How well you can hold the part is perhaps the biggest factor in how fast you can cut.
 With insert tooling, the carbide is affixed to the tool body by the use of gibs and screws instead of being brazed / welded on. There are two basic types: dedicated insert heads and universal insert heads. With dedicated heads the body is machined to match the profile of the insert to provide support. With universal insert heads the body is open and does not provide support; instead, there is a “backing plate” that is profiled the same as the insert to provide support. With the Universal design you are able to use the same head with multiple profiles by changing the backing plate and inserts. The Universal design is generally more expensive since it consists of an additional backing plate and the inserts are in general larger to accommodate a variety of profiles. We would be happy to help you select the style that will work best for you.
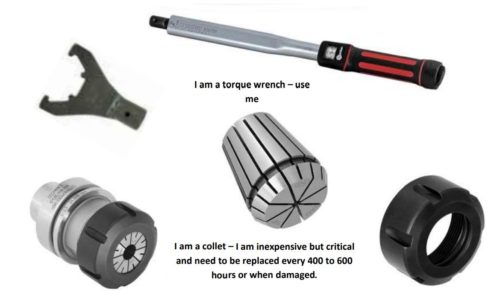 • Over-tightening of the collet and collet nut is a common mistake. Most operators assume that the tighter the better – this is not true and can lead to premature tool and collet wear and tool breakage. Collets are the most misunderstood and overlooked part of the CNC, often the cause of poor finish, short tool life, and unnecessary machine wear. Collets are made of spring steel and are subject to distortion when put under undue pressure. It is highly recommended that collets be tightened to manufacturers’ specifications with the use of a torque wrench